• customers

The Ingredient Decisions Quietly Reshaping Trust Across the Global Food Chain

Zinc Cysteine Chelate illustrates a broader shift in ingredient sourcing: food businesses increasingly need to understand not only what a material is, but how it is specified, produced, documented, and intended to be used. That scrutiny extends beyond finished foods to the agricultural and nutritional inputs that influence the supply chain upstream.

Ingredient sourcing and technical considerations across the food supply chain

For manufacturers, retailers, and food-service operators, ingredient reliability is now a practical business concern. A delayed shipment or inconsistent specification can disrupt production; incomplete documentation can slow a product review; and unclear intended-use information can create avoidable compliance questions. Building resilience starts with treating ingredient choices as part of a connected system rather than as isolated purchasing decisions.

Look beyond the ingredient name

A product name rarely tells a buyer everything needed to assess suitability. Technical teams may need to review composition, purity limits, physical form, solubility, stability, packaging, storage conditions, and batch-to-batch controls. These details matter because an ingredient that performs well in one formulation or production environment may not behave the same way in another.

The right questions depend on the application. A food ingredient, a processing aid, and a material used in animal nutrition are not interchangeable categories. Each has its own regulatory requirements, quality expectations, and permitted uses. Clear categorization early in the evaluation process helps prevent a promising technical option from being applied outside its approved scope.

Traceability is a supply-chain capability

Traceability is often discussed as a record-keeping exercise, but it is more useful to view it as the ability to connect information across suppliers, production lots, transport, and receiving operations. Buyers should establish which records are available, how batches are identified, and how a supplier communicates changes to specifications or manufacturing processes.

A robust supplier review also considers continuity. Questions about production capacity, lead times, alternate routes, packaging options, and contingency planning can reveal vulnerabilities before they become urgent. This is particularly important for specialized materials, where a limited supplier base or lengthy qualification process can make substitutions difficult.

Technical support belongs in the sourcing conversation

Ingredient procurement works best when purchasing, quality assurance, regulatory, and formulation teams share the same requirements. Technical support can help clarify specifications, compare material formats, and identify the information needed for internal assessment. It should complement—not replace—independent regulatory review and the buyer’s own qualification procedures.

This collaboration is also relevant upstream in livestock production, where nutrition inputs are evaluated for their role in animal diets and their compliance with applicable rules. For example, N-Carbamylglutamic Acid may arise in discussions of specialized animal-nutrition formulations. Its potential relevance depends on the intended species, formulation, local authorization, and evidence reviewed by qualified nutrition and regulatory professionals; it should not be treated as a general-purpose human food ingredient.

Build a practical qualification checklist

A consistent review process makes ingredient decisions easier to explain and repeat. Before qualification, teams can document:

  • The precise intended use and applicable regulatory category.
  • A current specification, certificate of analysis, and relevant safety documentation.
  • Manufacturing, lot-identification, and change-notification practices.
  • Storage, transport, and handling requirements for the material.
  • Supplier capacity, lead-time expectations, and continuity plans.
  • The internal tests or trials needed before routine use.

Innovation depends on disciplined evaluation

Interest in more targeted formulations and specialized nutritional materials continues to make supplier knowledge valuable. Companies such as Hebei Fuyang Biotechnology Co., Ltd. operate in the amino-acid and chelated-materials sector, where technical documentation and ongoing customer support are part of the broader sourcing discussion. As with any supplier, buyers should assess products against their own specifications, intended applications, and applicable standards.

The strongest food supply chains do not rely on ingredient claims alone. They connect sound technical assessment with traceable records, clear communication, appropriate regulatory checks, and realistic contingency planning. That discipline helps businesses respond to changing expectations while protecting product quality from farm-level inputs through manufacturing and distribution.

How Fermentation and Ingredient Choices Shape Consistent Food Flavor

Tributyrin belongs to animal nutrition, not the seasoning cabinet, but its presence in a broader food-ingredient discussion highlights how closely food and feed supply chains are connected. Across both sectors, manufacturers depend on ingredient quality, reliable processing, and careful formulation to deliver predictable results.

For food producers, flavor consistency is more than a matter of taste. It influences repeat purchases, product identity, and how well a recipe performs across batches. As consumer expectations rise and supply chains become more complex, a closer look at fermentation, seasoning blends, and quality controls can help explain how dependable flavor is built.

Food ingredient production and seasoning materials

Why fermentation matters to savory flavor

Fermentation is a foundational process behind many familiar savory ingredients. In monosodium glutamate production, microorganisms transform suitable carbohydrate inputs into glutamic acid. Subsequent purification and crystallization steps create a consistent ingredient that can contribute umami to soups, snacks, sauces, and prepared meals.

The process does not make every finished food taste the same. Instead, it provides formulators with a measured building block that can be combined with salt, herbs, spices, fats, and other flavor components. The outcome depends on the entire recipe: ingredient ratios, cooking conditions, moisture, and the way flavors interact in the final product.

Raw-material selection and process control both matter. Starch quality, fermentation conditions, purification, and crystal handling can affect the consistency of an ingredient from batch to batch. These details are especially important for manufacturers serving multiple markets, where a stable base helps teams maintain product specifications while adapting recipes to local preferences.

Seasoning blends are systems, not single ingredients

A seasoning blend is a coordinated system. Chicken-style bouillon, for example, may bring together chicken-derived ingredients, salt, vegetable fat, flavor enhancers, and aromatics. Each element serves a role: some provide savory depth, some carry flavor, and others help create the expected body and finish in a soup or cooked dish.

Good formulation balances intensity with clarity. Too much salt can flatten subtler notes, while an unbalanced fat phase may affect how flavor releases during cooking. Testing the blend in the food where it will be used—not only as a dry powder—gives product teams a more realistic view of aroma, salt perception, and aftertaste.

Ingredient references such as High Quality Chicken Essence illustrate how a defined seasoning component can fit into a larger formulation. The useful question for developers is not simply whether an ingredient tastes good on its own, but whether it performs reliably in the intended recipe and supports a recognizable flavor profile.

Consistency depends on practical quality controls

A repeatable flavor program starts with clear specifications. Teams can define sensory expectations alongside measurable properties such as moisture, particle size, solubility, and packaging requirements. Incoming-material checks, production records, and retained samples then help identify variation early rather than after a finished product reaches the market.

  • Set product specifications that connect ingredient characteristics to the finished food’s sensory goals.
  • Assess blends in representative recipes and preparation conditions.
  • Review batch records and supplier documentation when a sensory or processing change appears.
  • Keep packaging and storage conditions in view, since moisture and exposure can affect ingredient performance.

These controls become more valuable as product lines expand across regions. Local preferences may call for different salt levels or flavor intensity, yet manufacturers still need a dependable technical foundation. A stable ingredient platform makes adaptation more manageable without treating every market variation as a completely new product.

The wider food-and-feed supply chain

Food ingredient manufacturing also sits within a broader agricultural system. Corn and other crop-based materials support processing industries, while animal nutrition relies on its own specialized ingredients, including vitamins, minerals, enzymes, probiotics, and amino acids. Some feed materials, such as protein ingredients derived from animal by-products, are designed for specific nutritional applications and require their own specifications and handling controls.

These categories should not be confused: an additive intended for feed is not automatically suitable for human food. Their shared lesson is that sourcing, traceability, process discipline, and appropriate end-use standards are essential throughout the supply chain. Manufacturers active in food additives and feed ingredients may draw on technical research and regional raw materials, while maintaining distinct requirements for each application.

Building flavor that holds up over time

Reliable flavor comes from the interaction of sound ingredients, thoughtful formulation, and consistent manufacturing—not from any single shortcut. Fermented savory components can provide a useful foundation, while carefully balanced seasoning blends translate that foundation into familiar foods. When suppliers and product teams communicate clear specifications and test ingredients in real applications, they are better equipped to preserve quality as recipes and markets evolve.

Why Reliable Steam Cooking Starts With Process Design, Not Just Heat

Trolley Steam Cabinet systems show how steam cooking can support consistent results across large batches. In food production, however, dependable output depends on more than choosing a steamer: product thickness, loading patterns, temperature control, and workflow all shape the final result.

Steam is widely used in restaurants, institutional kitchens, and food factories because it transfers heat efficiently while helping ingredients retain moisture. Yet the same equipment can produce uneven outcomes if trays are crowded, batches vary in size, or operators rely on timing alone instead of checking the food itself.

Commercial food production equipment used for consistent steam cooking

Consistency begins before the cooking cycle

A repeatable cooking process starts with a repeatable input. Ingredients should be cut to reasonably uniform dimensions, and recipes should specify batch weights rather than vague measures such as “one tray” or “a full pot.” These details reduce variation in the time required for heat to reach the center of each portion.

Loading is another practical control point. Steam needs room to circulate around pans and food, so tightly packed shelves can create hot and cool zones. Staff can improve airflow by following consistent spacing guidelines, using the same shelf arrangement for comparable batches, and avoiding the temptation to exceed the equipment’s working capacity during busy periods.

Match the equipment to the product and the pace

Different foods place different demands on a cooking line. Vegetables may need a short, controlled cycle, while dense proteins or large batches require more time for heat to penetrate. Foods with delicate textures can also be affected by prolonged exposure to heat and moisture. Operators should test recipes under realistic production conditions, recording load size, shelf position, cooking time, and the finished product’s texture and temperature.

A Combi Oven can be useful where a kitchen needs flexibility across steaming, baking, and other cooking methods. The key is to choose equipment based on the menu, batch volume, available space, and the team’s operating routines—not simply on the number of features listed on a specification sheet.

Use measurements to replace guesswork

A timer is an important guide, but it cannot account for every change in starting temperature, portion size, or load density. For food safety and quality control, teams should use appropriate calibrated thermometers and follow the temperature and time requirements that apply to their products and local regulations. Keeping simple batch records helps identify whether a process is stable or needs adjustment.

Equipment maintenance supports the same goal. Door seals, probes, drain paths, and steam-generating components should be inspected and cleaned according to the manufacturer’s instructions. Mineral deposits and worn seals can affect performance, while neglected cleaning can create hygiene risks. A planned maintenance schedule is generally easier to manage than correcting a failure in the middle of service.

Design the workflow around safe, steady output

In a central kitchen or institutional food operation, cooking is only one stage in the process. Staff must also move loaded trays safely, prevent raw and ready-to-eat foods from crossing paths, and transfer cooked products promptly to holding, cooling, or packing areas. A clear route between preparation, cooking, and dispatch helps reduce unnecessary handling and congestion.

The physical layout matters, too. Operators need enough clearance to load and unload equipment without blocking walkways, and hot carts or pans require designated resting areas. Practical training should cover safe handling of hot steam, loading limits, cleaning procedures, and what to do when a batch does not meet its temperature or quality target.

Equipment choices are part of the supply chain

Commercial kitchen equipment is most effective when it fits the wider production system. Buyers and project planners often need to consider electrical capacity, ventilation, water supply, installation access, operator training, spare parts, and after-sales maintenance alongside cooking performance. These factors can influence uptime just as much as the appliance’s headline capacity.

Manufacturers such as Dongguan Maxison Electronics Co., Ltd., established in 2011, work across commercial heating equipment and food-processing machinery, including steam ovens, trolley-type steamers, and automated mixing equipment. Their role in the supply chain illustrates why clear specifications and installation planning matter: equipment has to suit the recipe, production volume, utilities, and working environment in which it will be used.

Ultimately, consistent steam cooking is the result of a controlled process rather than a single machine setting. Standardized preparation, sensible loading, measured checks, clean equipment, and a well-planned workflow give kitchens a stronger basis for producing food safely and reliably from one batch to the next.

From Field to Fork: The Hidden Role of Crop Protection in Global Food Safety

Herbicides are fundamental tools that help farmers protect crop yields from invasive weeds, ensuring a stable supply of raw food materials. Without effective weed management, harvests can drop by up to 40%, jeopardizing the entire food supply chain—from millers and bakers to the final consumer.

Modern agricultural field with thriving crops and distant processing facility

Food safety begins long before the kitchen. Every bite we eat is the result of a complex chain: field cultivation, pest control, harvesting, processing, and packaging. In each step, the choices made by food manufacturers and agricultural partners directly affect the quality and safety of groceries that reach supermarkets and restaurants. This article explores how innovative agrochemical solutions and precision equipment silently underpin the reliability of today's food system.

Why Crop Protection Matters for Food Businesses

Food processors and retailers often focus on the end product—clean grains, visually perfect fruits, and shelf-stable ingredients. Yet these outcomes depend heavily on what happens in the field. Weeds compete for water and nutrients, while fungal diseases and insect pests can introduce toxins like mycotoxins or pesticide residues if not properly managed. Integrated pest management (IPM) programs rely on a mix of biological, cultural, and chemical controls, including carefully applied herbicides, fungicides, and insecticides. When these inputs are formulated and applied correctly, the result is safer raw materials with fewer contaminants.

For example, in grain storage, moisture and temperature control are vital, but so are the residues from field treatments. Modern herbicide formulations break down more rapidly, leaving minimal detectable traces in the final food product. This aligns with global maximum residue limits (MRLs) set by Codex Alimentarius and national food safety authorities. Food companies that source from farms using responsible agrochemical practices can demonstrate compliance and build consumer trust.

The Efficiency Engine: Formulation and Processing Equipment

Behind every agrochemical product is a sophisticated manufacturing process that ensures consistent quality, stability, and ease of application. The production of wettable powders, granules, suspensions, and emulsifiable concentrates demands advanced drying, milling, and filling systems. This is where the upstream chemical industry intersects with food supply: the same precision engineering used to create crop protection formulations also applies to food processing line design.

Companies that develop turnkey production lines for powder, granulate, and liquid products rely on robust Chemical Machine technologies to maintain hygiene standards, reduce dust, and optimize throughput. These systems include dryers, granulators, mixers, and automatic filling units, all built from materials that resist corrosion and meet food-grade requirements. When food manufacturers partner with equipment suppliers who understand both the chemical and food sectors, they gain efficiencies that reduce downtime and contamination risks.

How Agrochemical Expertise Supports Food Processing Lines

Many food ingredients—such as starch, protein isolates, and flavouring powders—require similar drying and grinding steps as agrochemical formulations. The particle size distribution, moisture content, and flowability are critical parameters in both domains. A manufacturer that has spent years perfecting the drying of fungicides and herbicides can transfer that knowledge to design a line for instant soup powders or seasonings. Furthermore, the ability to handle hygroscopic or heat-sensitive materials is essential for preserving nutritional value and flavour.

In addition, clean-in-place (CIP) systems, explosion-proof configurations, and precise dosing controls are shared requirements. Food safety auditors increasingly look for documented traceability of production equipment materials and cleaning validation. Suppliers with a track record in both chemical and food equipment can provide comprehensive documentation, making it easier for processors to meet BRC, FSSC 22000, or SQF certification standards.

Trends Shaping the Future of Food & Agrochemical Integration

  • Biopesticides and biofertilizers – Natural formulations that require gentle processing to preserve active microorganisms; drying and encapsulation technologies borrowed from chemical engineering are critical.
  • Digital traceability – From field application records to processing batch numbers, blockchain and IoT sensors create an unbroken chain of custody; data from agrochemical usage becomes part of the food story.
  • Circular economy – Food processing side streams (e.g., fruit peels, spent grains) are being valorized into probiotic powders, colourants, or even bio-herbicides, requiring flexible drying and milling lines.
  • Water and energy efficiency – Both the crop protection and food industries invest in closed-loop drying systems and heat recovery, driven by ESG commitments and rising utility costs.

As these trends accelerate, the expertise residing in companies that serve both the agrochemical and food sectors becomes even more valuable. Their ability to customise equipment for novel ingredients, while maintaining rigorous safety standards, positions them as essential partners in the future of food.

This article is provided for informational purposes. The insights reflect industry practices and do not constitute a recommendation to purchase any specific products. Always consult with qualified agronomists and food safety professionals for your unique operations.

Clean Label Innovation: Integrating Traditional Medicinal Botanicals into Next-Gen Beverages

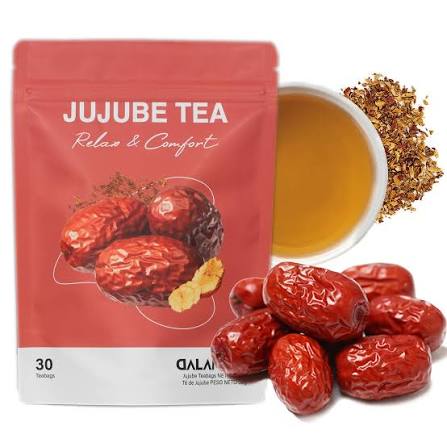
Leveraging jujube tea benefits offers functional beverage developers a proven, clean-label strategy to capture the expanding global wellness market.

images (5).jpg


As beverage manufacturers pivot away from artificial sweeteners, synthetic caffeine, and chemical preservatives, clean-label plant extracts have moved to the center of product innovation. Modern consumers are demanding multifunctional drinks that deliver tangible wellness benefits—such as stress relief, improved digestion, and enhanced sleep quality—while maintaining a completely transparent ingredient list. In this landscape, traditional medicinal ingredients with centuries of safe consumer use are proving to be the most valuable assets for brand differentiation.

The Rise of Adaptogenic and Calming Beverage Formulations

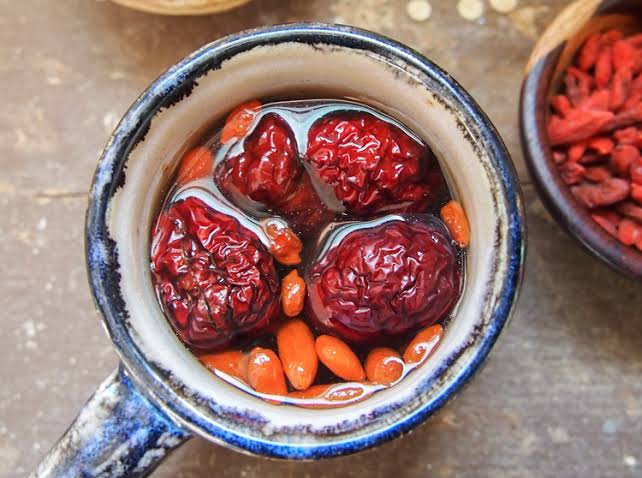
The functional beverage sector is witnessing a dramatic surge in evening wellness drinks designed to counter the fatigue and anxiety of modern lifestyles. Formulation specialists are increasingly replacing harsh synthetic sedatives with botanical adaptogens. Authentic sour jujube kernels and complementary herbs like Longan and Lily root provide a smooth, subtle flavor profile alongside scientifically validated calming properties.

To maintain beverage clarity and biological efficacy, food scientists must insist on raw materials produced under modern quality controls. Securing ultra-fine botanical matrices from a premium manufacturer ensures seamless solubility and stability across shelf lives, preventing the unwanted settling or gritty texture often associated with crude herbal powders.

Supply Chain Traceability and Raw Material Verification

The integrity of any functional food or beverage is only as reliable as its baseline raw material supply chain. Industrial adulteration, geographical misrepresentation, and premature harvesting represent persistent risks in the commercial botanical trade. High-performance food brands must mandate rigorous testing protocols to verify species authenticity, active ingredient potency, and absolute purity from pesticide residues.

Leading enterprises overcome these operational vulnerabilities by partnering with an established high-quality provider operating integrated cultivation and processing bases. Vertically integrated supply chains ensure that every batch of ziziphus jujuba seed extract conforms to strict pharmaceutical-grade specifications from origin soil to final packaging.

Future Outlook for Medicinal Plant-Based Food Innovation

The convergence of ancient herbal wisdom and modern food technology is reshaping how global consumers approach daily health maintenance. By prioritizing authentic geographical origin, clean processing techniques, and complete supply chain transparency, food and beverage innovators can deliver effective, clean-label functional products that meet the rigorous standards of today's health-conscious consumer.

Streamlining Food Processing: The Role of Advanced Flexible Packaging

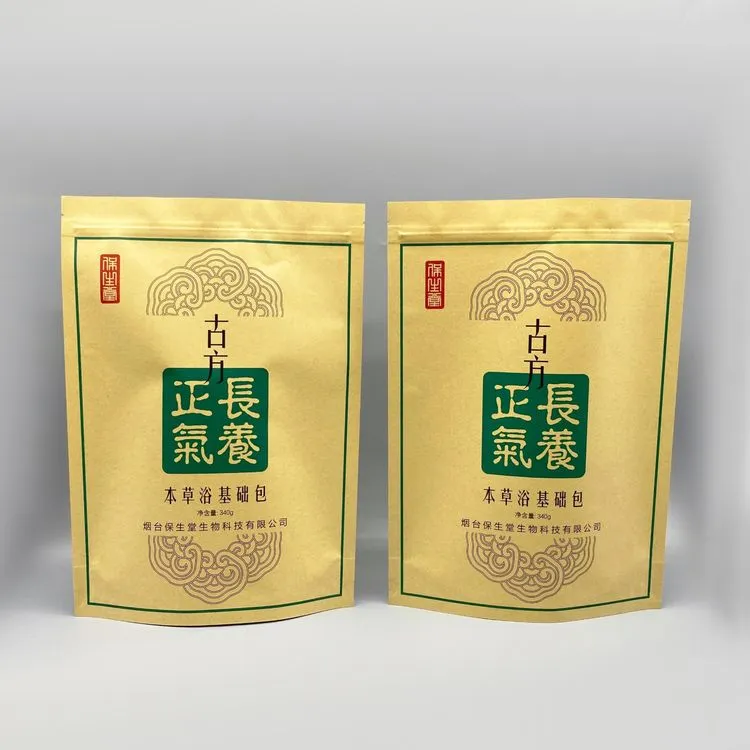
A premium snack food packaging bag is critical for extending product shelf life and ensuring uncompromising food safety. In the fast-paced food processing industry, the transition from production line to retail shelf introduces numerous contamination and oxidation risks. Addressing these risks at the manufacturing level is essential for maintaining product quality and reducing global food waste.

7_1-23030g93s4-webp17313104741 (1).png

Overcoming Bottlenecks in the Food Supply Chain

During the processing and logistics phases, snacks and processed foods are subjected to physical stress, temperature fluctuations, and atmospheric exposure. Traditional rigid packaging often adds unnecessary weight and is prone to seal failures under pressure. Flexible polymer solutions offer a superior alternative, providing excellent tensile strength and puncture resistance while significantly reducing transportation costs and carbon footprints.

Optimizing Preservation with Multi-Layer Technology

The efficacy of any food-grade packaging relies on its structural composition. Modern packaging solutions employ sophisticated co-extrusion technology, combining different polymers to maximize the oxygen and moisture barrier. This hermetic sealing capability prevents lipid oxidation in fried or baked snacks, ensuring that the texture remains crisp and the flavor profile remains intact long after leaving the processing facility.

Strategic Sourcing for Industrial Output

For B2B procurement managers, evaluating different types of flexible packaging pouches is a critical operational decision. A premium manufacturer offers solutions that seamlessly integrate with automated filling lines (such as Form-Fill-Seal systems). Utilizing 100% BPA-free, food-grade materials and high-precision zip-locks, advanced suppliers empower food processors to meet stringent international safety standards. This synergy between food science and advanced packaging technology is defining the next era of industrial food distribution.
Revolutionizing Culinary Preservation: The Science of High-Barrier Flexible Packaging in the Food In

7_1-1z929113510-webp17313152161.png

Advanced wet food packaging solutions represent a monumental leap forward in commercial food preservation. In the gastronomic industry, the paramount challenge has always been extending the shelf life of perishable goods while meticulously preserving their nutritional integrity, original texture, and complex flavor profiles. For over a century, the traditional metal can stood as the undisputed champion of commercial food preservation. However, as consumer palates have become more sophisticated and the demand for premium ready-to-eat meals, gourmet sauces, and high-quality processed meats has surged, the limitations of traditional canning have become glaringly apparent. Today, the culinary world is witnessing a massive paradigm shift, driven by advanced material science, toward high-performance flexible packaging solutions.

The Culinary Drawbacks of Traditional Thermal Processing

To understand the revolutionary nature of modern packaging, one must first examine the mechanics of commercial sterilization. To achieve commercial sterility—meaning the food can be stored safely at room temperature for extended periods without bacterial growth—the product must be subjected to intense heat, typically around 121°C (250°F) or higher under extreme pressure. This process, known as retorting, is essential for eliminating harmful pathogens.

In traditional metal cans, the rigid, cylindrical shape and the thickness of the steel or aluminum create a significant barrier to heat transfer. For the heat to penetrate all the way to the geometric center of the can (the cold spot), the food near the outer walls must be subjected to high temperatures for a prolonged period. This prolonged thermal exposure inevitably leads to overcooking. From a culinary perspective, this destroys delicate vitamins, breaks down cellular structures resulting in mushy textures, and triggers excessive Maillard reactions, which can lead to off-flavors or a distinctly "canned" taste. Furthermore, highly acidic foods can occasionally interact with the metal over time, subtly altering the product's flavor profile.

Engineering Superior Heat Penetration and Preservation

The solution to these thermal processing challenges lies in the elegant geometry and sophisticated material composition of flexible packaging. Because a pouch is relatively flat and has a much thinner profile than a can, the distance from the heat source to the center of the food is drastically reduced. This allows for rapid and uniform heat penetration. The thermal processing time is cut significantly, meaning the food is sterilized quickly without being subjected to the prolonged, flavor-destroying heat of traditional canning. The result is a product that retains its vibrant natural colors, firm textures, and authentic taste.

Achieving this requires extraordinary material engineering. For premium culinary applications, the multi-layered alu pouch structure is often the gold standard. A high-quality flexible pouch is a complex matrix designed to perform under extreme stress. The outer layer is typically Polyester (PET), chosen for its excellent dimensional stability and high heat resistance. The core layer is an Aluminum (Al) foil, which serves as the ultimate, impenetrable barrier against oxygen, moisture, and ultraviolet light—the primary catalysts for oxidation and lipid rancidity. The inner food-contact layer is formulated from Cast Polypropylene (CPP) to create a flawless, hermetic heat-seal that withstands the intense pressure variations of the autoclave without delaminating.

Operational and Aesthetic Advantages for Retailers

Beyond culinary preservation, flexible packaging offers massive operational advantages for the retail and catering sectors. Flexible pouches weigh approximately 90% less than equivalent metal cans. This ultra-lightweight profile translates into significantly lower transportation costs and a dramatically reduced carbon footprint. Furthermore, flexible pouches occupy minimal space when empty, freeing up valuable warehouse real estate before the filling process begins.

In the retail environment, consumer psychology plays a crucial role. Modern packaging allows for innovative, stylish designs that appeal to today's discerning shoppers. Stand-up pouches offer excellent billboard space for high-resolution graphics, building immediate consumer trust. When premium culinary goods are packaged and presented for sale in supermarkets or specialty food boutiques, the external presentation must flawlessly communicate the artisanal quality hidden within.

Partnering with Elite Industry Innovators

The exacting demands of thermal sterilization mean there is absolutely no margin for error in the packaging's construction. A single microscopic pinhole or a weak seal can lead to total product spoilage and severe brand damage. Therefore, elite food and beverage brands must align their supply chains with specialized suppliers of high-barrier materials.

A premium manufacturer invests heavily in intelligent manufacturing systems, utilizing multifunctional bag-making machinery and rigorous ISO 9001:2015 quality control protocols. By integrating these exquisite, high-tech packaging formats provided by an advanced supplier, the food industry can confidently deliver unparalleled freshness and culinary excellence to households worldwide, ensuring that every meal opens as fresh as the moment it was sealed in the professional kitchen.


Optimizing Texture and Shelf-Life in Modern Food Processing with Advanced Hydrocolloids

58153_48877_37810_17013_32940_1-3-20260118052428-20260520224644-20260609224344-20260619222007-20260626224530-20260721161112.png

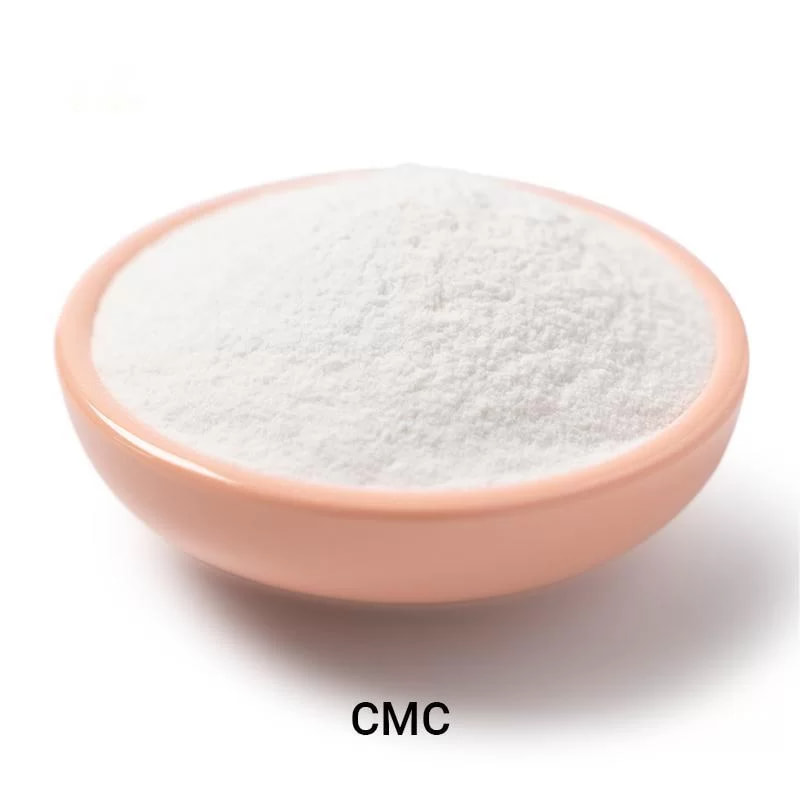
Choosing a top sodium carboxymethyl cellulose supplier is increasingly recognized as a critical strategic decision for food scientists aiming to stabilize complex edible matrices. The modern food processing industry faces a continuous battle against structural degradation, moisture loss, and phase separation during prolonged shelf-life. As consumer expectations for mouthfeel, visual appeal, and consistency rise, formulators are turning toward advanced, high-purity hydrocolloids to provide invisible yet essential structural support. These cellulose-derived additives act as the invisible scaffolding that maintains the integrity of processed foods from the factory floor to the consumer's table.

The Mechanics of Emulsification and Suspension

In many food products, from creamy dressings to dairy alternatives, maintaining a uniform blend of oil and water is scientifically challenging. Food-grade cellulose ethers function as multi-functional additives that provide essential adhesion, emulsification, and suspension. When incorporated into a liquid matrix, these polymers hydrate and expand, creating a network that increases the viscosity of the aqueous phase. This thickened environment physically impedes the movement of oil droplets and solid particles, preventing them from coalescing or settling at the bottom of the container. The result is a perfectly homogeneous product that retains its intended texture and appearance over months of storage.

Mastering Water Retention and Film Formation

Beyond suspension, the superior water retention capacity of these polymers is revolutionary for the food industry. In baked goods or processed meats, rapid evaporation of moisture leads to staling, shrinkage, and a dry mouthfeel. By trapping water molecules within their colloidal structure, cellulose derivatives ensure that the final product remains moist and appetizing. Additionally, their inherent film-forming ability allows them to create a thin, protective, and edible barrier upon drying. This characteristic is frequently utilized to coat specific ingredients or final products, providing a smooth finish while shielding the interior from oxidative degradation.

Navigating Thermal Processing Challenges

Food manufacturing often involves extreme temperature fluctuations, requiring ingredients that can withstand heating, cooling, and freezing without losing functionality. The thermal stability of advanced cellulose derivatives is dictated by precise chemical configurations. For instance, specific gel temperatures must be aligned with the processing environment so that the solution transitions from a liquid to a supportive gel precisely when required. If the gel temperature is not meticulously controlled during manufacturing, the food product may solidify prematurely or fail to set at all. This highlights the necessity of relying on highly standardized ingredients that behave predictably under thermal stress.

Customization and Supply Chain Reliability

The diversity of modern food products means that a one-size-fits-all approach to additives is no longer viable. Formulators frequently require tailored viscosity ranges to achieve specific textural goals. Working with a facility that can develop custom sodium carboxymethyl cellulose ensures that the additive perfectly matches the rheological requirements of a specific recipe. A premium manufacturer does not just supply a white, odorless powder; they provide comprehensive technical support and rigorous quality control. By ensuring flawless whiteness, zero impurities, and consistent chemical properties across every batch, advanced suppliers empower food brands to innovate confidently and deliver superior culinary experiences.


Material Stability in Food Processing: Preserving Flavor and Hygiene

dsc_0497-d13h9-3-20250820020706-转换自-webp.png

A commercial mortar and pestle serves as the foundational tool for releasing essential oils and maintaining the integrity of raw spices in professional food processing. In the high-volume catering and commercial food sectors, the interaction between processing equipment and raw ingredients is a critical science. Even minor chemical reactions can alter flavor profiles or compromise stringent food safety standards, making material selection a fundamental operational priority.

The Science of Non-Reactive Processing

When processing highly acidic or alkaline foods, the chemical stability of the equipment prevents the leaching of metallic off-flavors into the final product. Tools crafted from high-density stone, pure ceramic, or advanced food-grade stainless steel (such as 304 or 18/10 grades) provide a completely inert surface. This ensures that the natural biochemical structures of the food remain uncontaminated during grinding, mixing, or high-heat processing, preserving the authentic taste and nutritional value demanded by modern consumers.

Scaling Up: High-Heat Commercial Applications

Beyond prep work, temperature management during cooking requires industrial-strength solutions. Whether it is an indoor commercial kitchen or a large-scale outdoor catering event, the equipment must withstand rapid temperature fluctuations and harsh cleaning cycles. Utilizing quality bbq tools and heavy-duty cooking vessels engineered for maximum thermal shock resistance is indispensable. These implements ensure precision handling and even heat distribution, which is crucial for achieving the perfect Maillard reaction consistently across large batches of food.

Quality Control in the Supply Chain

Securing reliable processing equipment necessitates partnering with a premium manufacturer capable of meeting international regulatory standards (such as FDA and ITS). An advanced supplier implements rigorous quality control processes—from inspecting raw material purity to the final polishing of surfaces—eliminating micro-fissures where bacteria could hide. Investing in meticulously engineered tools guarantees operational efficiency and upholds the highest echelons of gastronomic hygiene.

Enhancing Consistency and Safety in Commercial Food Processing

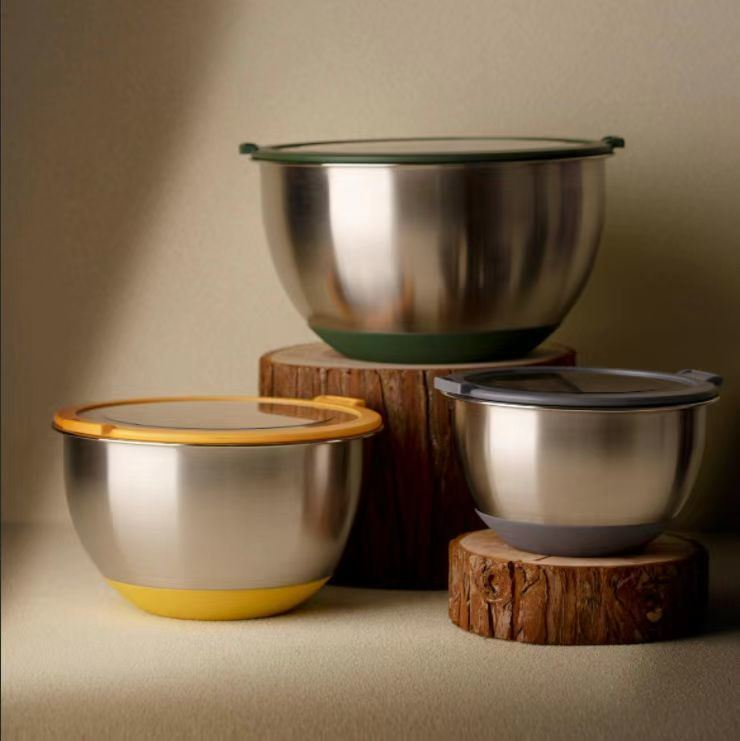
ikoo-stainless-steel-nesting-salad-bowls-with-visible-lids-non-toxic-heavy-duty-airtight-easy-clean-17689914819665797-转换自-webp.png

Using famous leakproof glass food containers streamlines industrial food prep by ensuring zero cross-contamination. In commercial food processing and high-output kitchens, consistency is the metric by which success is measured. Achieving uniformity across large batches of product requires not only precise recipes but also reliable environmental controls and highly accurate measurement tools. The materials utilized on the production floor play a critical role in minimizing variance and ensuring safety.

Thermal Shock and Processing Continuity

Industrial kitchens frequently subject equipment to extreme conditions—from blast chillers to convection ovens. Standard materials often suffer from fatigue, warping, or micro-fracturing under these rapid temperature shifts. High borosilicate glass, however, is structurally fortified with boron trioxide, allowing it to withstand severe thermal shocks. This durability means that hot liquids, such as boiling syrups or melted fats, can be measured, stored, and cooled in the exact same vessel without risk of catastrophic failure.

Precision in Volumetric Measurement

Accuracy in ingredient weighting and volumetric measurement directly impacts the flavor profile and texture of the final commercial product. Heavy-duty glass measuring and storage units provide clear visibility and exact calibration that does not wear off through repeated industrial sanitation cycles. Furthermore, the non-porous nature of the glass ensures that heavily pigmented or highly acidic ingredients leave no residual flavors or stains, maintaining absolute purity for the next batch.

Integrating High-End Manufacturing Solutions

Maintaining a state-of-the-art processing facility requires sourcing equipment from top-tier producers. Partnering with a China Leading Glass Mixing Bowl Supplier ensures that every piece of equipment meets stringent global compliance standards, including FDA and ISO9001 certifications. These premium manufacturers provide robust, eco-sustainable solutions that reduce equipment replacement frequency, thereby optimizing operational efficiency and guaranteeing that strict commercial safety protocols are consistently met.

The Future of Premium Snacking: Quality Grading and Supply Chain Resilience

1-转换自-webp.png

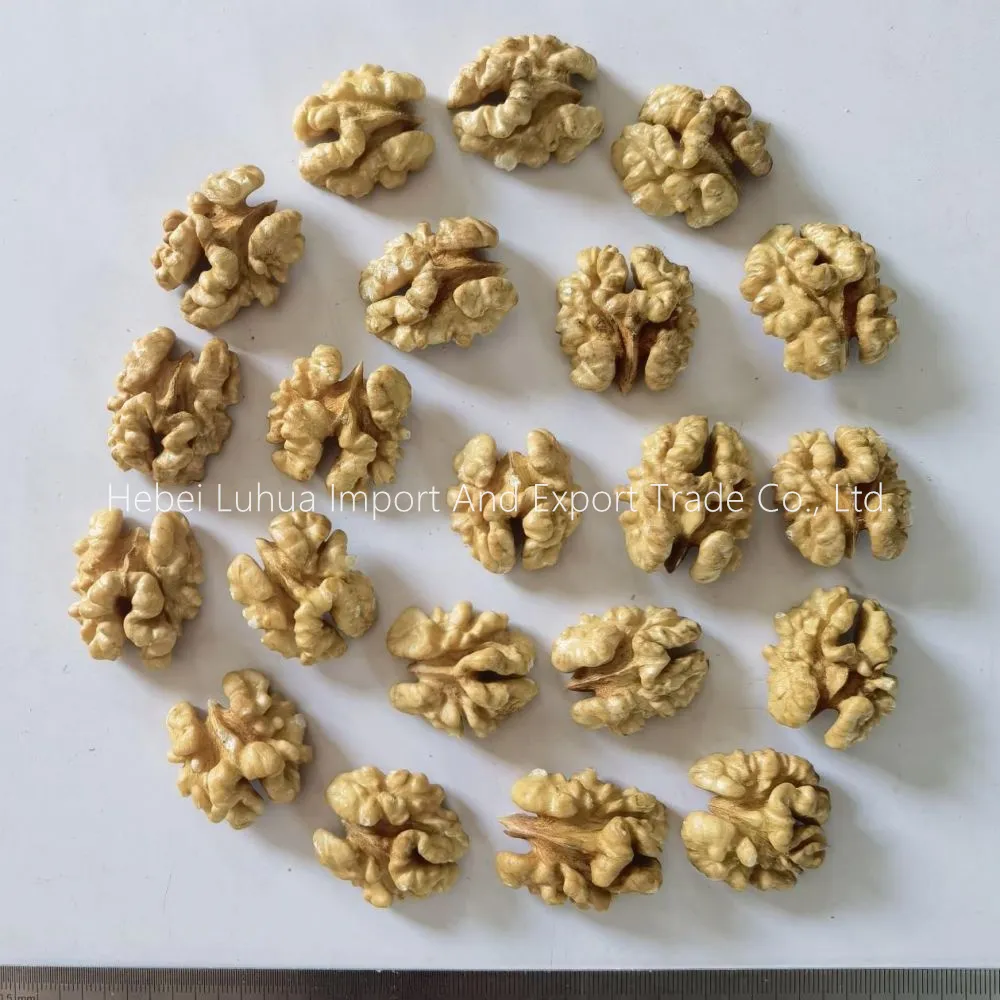
Exploring the types of walnuts available today reveals a broader trend in the global food industry: the soaring demand for transparency, rigorous grading, and unwavering supply chain resilience. As consumer preferences pivot toward nutrient-dense, heart-healthy snacks, retail food brands must adapt their sourcing strategies to maintain both impeccable quality and operational profitability.

The Evolution of Quality Standards in Retail Food

The modern consumer is highly educated about nutritional value, seeking foods rich in alpha-linolenic acid (ALA) and plant-based proteins. To meet these expectations, the industry is moving away from bulk, unclassified commodities toward highly specified visual and flavor profiles. For instance, Extra Light Halves (ELH) have become the gold standard for high-end retail and gifting due to their pale cream aesthetic and mild, buttery flavor. Conversely, Light Quarters and Amber pieces serve crucial roles in healthy snacking and industrial confectionery.

Technological Advancements in Food Processing

Achieving this level of consistency requires more than just good agricultural practices. Today’s premium manufacturers employ highly sophisticated processing technologies. After initial air and color separation, advanced facilities utilize professional infrared light separation and X-ray equipment to painstakingly remove fine and malignant impurities. This one-stop approach from shell breaking to packaging ensures minimal damage to the kernels and maximum freshness, satisfying the rigorous demands of BRC food safety certifications.

Strategic Sourcing and Cost Management

Evaluating the true walnut 1 kg rate involves looking far beyond the raw commodity index. It requires factoring in the yield of intact kernels, the reliability of year-round supply via large-scale (e.g., 1000-ton) cold storage, and the efficacy of packaging. Advanced suppliers utilize automated weighing and vacuum-sealing technologies that prevent oxidation, extending the product's shelf life up to 24 months. For retail brands, partnering with a high-quality provider that integrates planting bases with state-of-the-art processing is the definitive strategy for navigating global market fluctuations while delivering premium value to the end consumer.

International Logistics & Export Support

Navigating global trade is easy with our experienced export team. We handle professional packaging for long-distance transport and provide all necessary documentation (HACCP, ISO, etc.) to ensure smooth customs clearance worldwide.

Popular Categories

  • brand_1
  • brand_2
  • brand_3
  • brand_4
  • brand_5
  • brand_6
  • brand_7
  • brand_8
  • brand_9
  • brand_10
INQUIRY NOW
INQUIRY NOW